Explore our core portfolio of cosmetic-grade and bio-industrial ingredients engineered to European and North American purity standards.
Trehalose (α-D-glucopyranosyl-1,1-α-D-glucopyranoside) is a naturally occurring non-reducing disaccharide composed of two glucose molecules joined by an α,α-1,1-glucosidic linkage. Known globally as the "Resurrection Sugar" due to its central role in the biological phenomenon of anhydrobiosis, Trehalose enables extremophile organisms—such as tardigrades, resurrection plants, and specialized yeasts—to survive complete desiccation and extreme thermal fluctuations without structural cell collapse.
In the global B2B chemical and biological ingredient markets, Trehalose has evolved from a rare, high-cost specialty molecule into a fundamental industrial bio-stabilizer, cosmetic active, and pharmaceutical excipient. The global industrial market for Trehalose, currently valued in excess of USD 600 Million, is projected to expand at a CAGR of 7.2% through 2032. This surge is driven by escalating demand across cosmetic formulation engineering, cellular cryopreservation, biopharmaceutical stabilization, and functional food processing.
Forms a stable amorphous glass phase (vitrification) upon drying, trapping tertiary protein structures and preventing irreversible denaturation during freezing or heat stress.
Triggers mTOR-independent cellular autophagy, accelerating the degradation of damaged cellular proteins and organelles for advanced anti-aging formulations.
As a non-reducing sugar, Trehalose does not undergo Maillard reactions with amino acids or proteins, ensuring total color, odor, and structural stability in formulations.
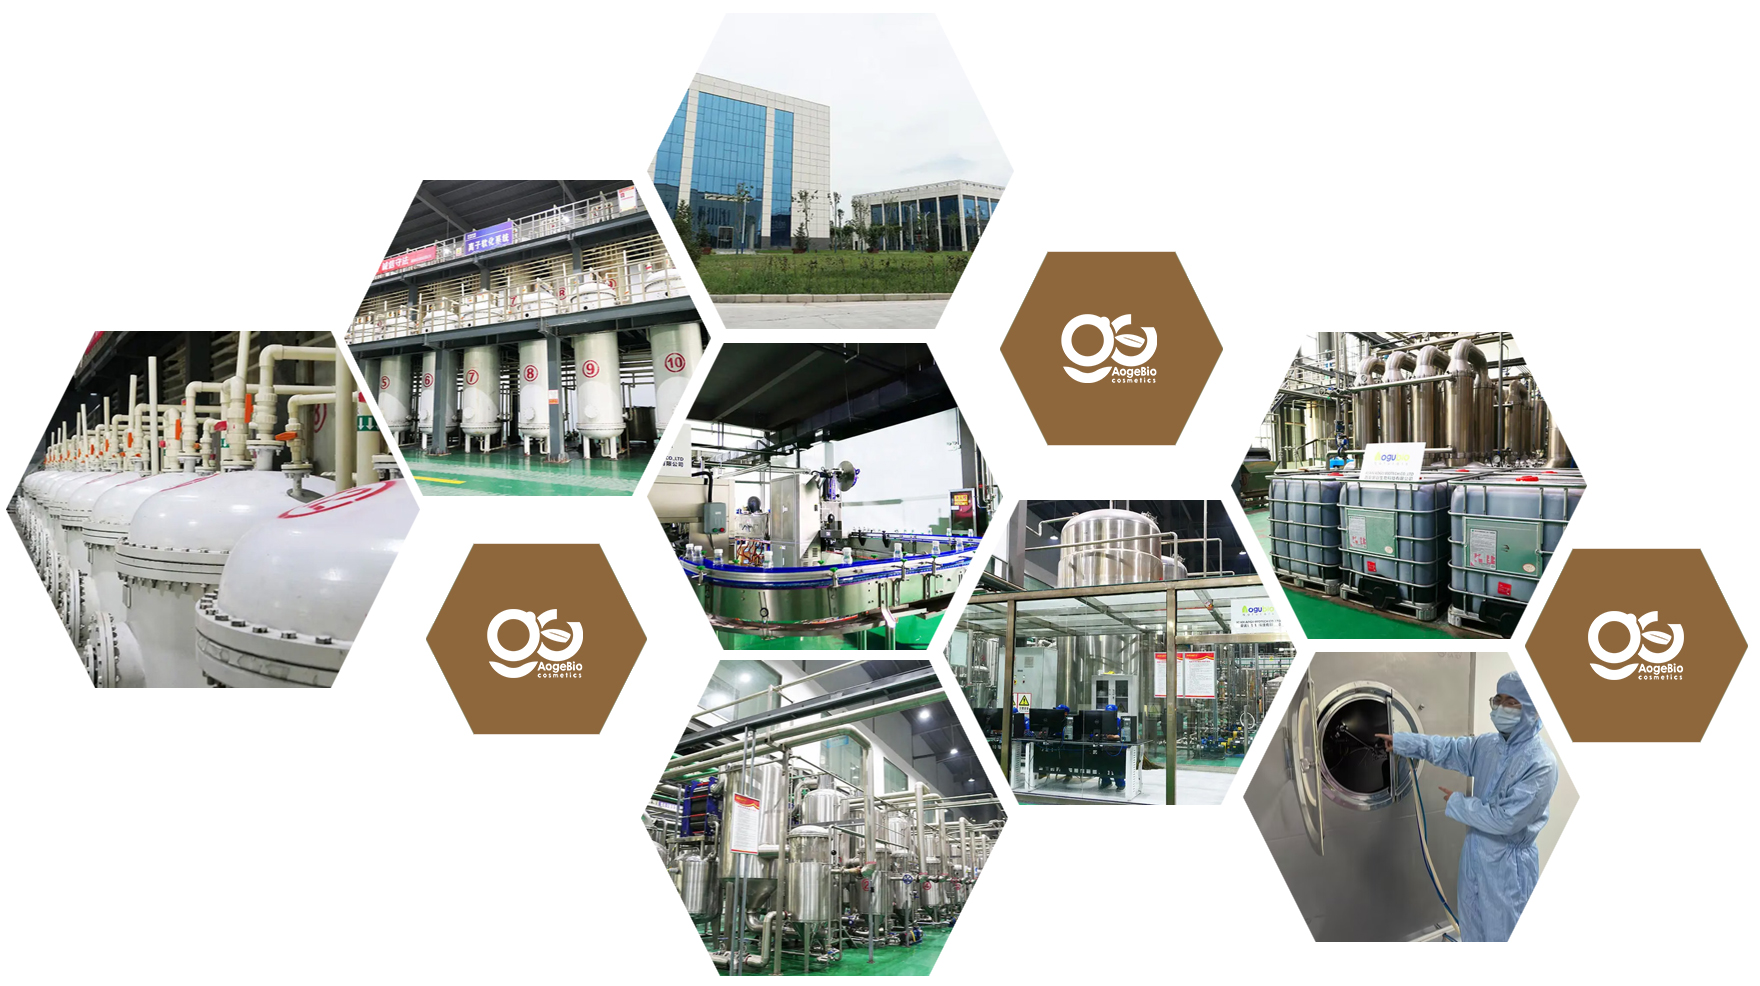
Founded in 2013 and headquartered in the prestigious high-tech zone of Xi'an, Xi'an Aoge Biotech Co., Ltd., along with its specialized subsidiaries Xi'an Imaherb Biotech Co., Ltd. and Xi'an Nahanutri Biotech Co., Ltd., has established itself as an authoritative global force in the cosmetic raw materials and fine chemical synthesis industry.
Our expansive cooperative factory, spanning over 66,667 square meters, is outfitted with multi-stage continuous enzymatic hydrolysis reactors, membrane ultrafiltration units, multi-effect vacuum evaporators, and ISO Class 7 cleanroom crystallization suites. This advanced infrastructure allows us to manufacture a wide array of premium cosmetic raw materials and specialized sugars. Our product lines service global cosmetic conglomerates, pharmaceutical formulators, and industrial biomanufacturers across North America, Europe, and the Asia-Pacific region.
To understand why custom Trehalose synthesis is critical for high-performance topical and pharmaceutical applications, formulators must analyze its thermodynamic profile against standard polyols and humectants like Glycerin, Hyaluronic Acid, and Sorbitol.
| Physicochemical Parameter | High-Purity α,α-Trehalose | Glycerin | Sodium Hyaluronate (HA) |
|---|---|---|---|
| Molecular Weight | 342.30 g/mol (Dihydrate: 378.33) | 92.09 g/mol | 100,000 – 1,500,000 Da |
| Glass Transition Temp (Tg) | High (~115°C dry state) | Extremely Low (-93°C) | Moderate (~60°C - dependent) |
| Reducing End Activity | Non-reducing (Zero Maillard Browning) | Non-reducing | Reducing Terminal Units |
| Autophagy Activation | Direct TFEB Pathway Trigger | None | None |
| Cellular Membrane Protection | Replaces lipid head-group bound H₂O | Osmotic Swelling Risk | Surface Hydration Film Only |
| Thermal Stability | Stable up to 100°C at pH 3.5 - 10.0 | Decomposes > 290°C | Degrades rapidly above 60°C |
When exposed to severe environmental stressors (such as UV irradiation, osmotic shock, or sub-zero freezing), traditional humectants fail to preserve cell membrane lipid bilayers. Trehalose directly coordinates with fluid phospholipid head groups, maintaining membrane fluidity and preventing protein phase-separation.
As a specialized B2B manufacturer, Aogebio LLC operates dual synthesis pathways tailored to specific customer application requirements. We eliminate traditional high-cost extraction methods by utilizing advanced enzymatic transglycosylation from food-grade corn starch.
1. Liquefaction & Debranching: Non-GMO starch slurries undergo enzymatic conversion using α-amylase and pullulanase.
2. Dual-Enzyme Conversion: Maltooligosyltrehalose synthase (MTSase) converts starch terminal ends into trehalose residues, followed by Maltooligosyltrehalose trehalohydrolase (MTHase) liberation.
3. Refinement & Decolorization: Active carbon adsorption, dual-bed ion-exchange resin chromatography for salt and heavy metal removal.
4. Crystallization: Controlled cooling crystallization producing high-purity α,α-Trehalose Dihydrate crystals.
• Custom Mesh Sizes: Standard crystalline (40-80 mesh), Fine Powder (100-200 mesh), and Micro-granulated formulations.
• Purity Standard Options: Cosmetic Grade (≥ 99.0%), Food/Nutraceutical Grade (≥ 98.0%), Bio-Pharma Endotoxin-Controlled Grade (≥ 99.5%, endotoxin < 0.05 EU/mg).
• Custom Blending & Packaging: 25 kg multi-wall moisture-barrier paper bags, 500 kg FIBC super-sacks, and private-label aluminum foil barrier pails.
Used in premium anti-pollution serums, anti-wrinkle creams, and scalp-soothing treatments. Protects skin fibroblastic cells from desiccation, reduces body odor by suppressing fatty acid oxidation, and protects formulation emulsions against freeze-thaw breakdown.
Acts as a critical lyophilization cryoprotectant for monoclonal antibodies (mAbs), mRNA lipid nanoparticles (LNPs), recombinant proteins, and live-attenuated viral vaccines, reducing cold-chain dependency.
Suppresses starch retrogradation in bakery products, preserves structural protein hydration in frozen seafood and meats, masks unpleasant bitterness in functional botanical extracts, and mitigates browning in fruit preserves.
Our in-house analytical testing facility utilizes state-of-the-art instrumentation including Ultra Performance Liquid Chromatography (UPLC), High-Performance Liquid Chromatography (HPLC), Gas Chromatography-Mass Spectrometry (GC-MS), and Inductively Coupled Plasma Mass Spectrometry (ICP-MS) for thorough quality control, ensuring raw materials consistently exceed international standards.
Relentless research into continuous enzyme biocatalysis and high-purity isolation techniques to keep our partners ahead in dynamic markets.
Every batch undergoes full-spectrum testing from raw starch sourcing to final crystal packaging, ensuring total batch-to-batch consistency.
Active integration of green chemistry practices, minimizing energy consumption and utilizing closed-loop water recycled filtration systems.
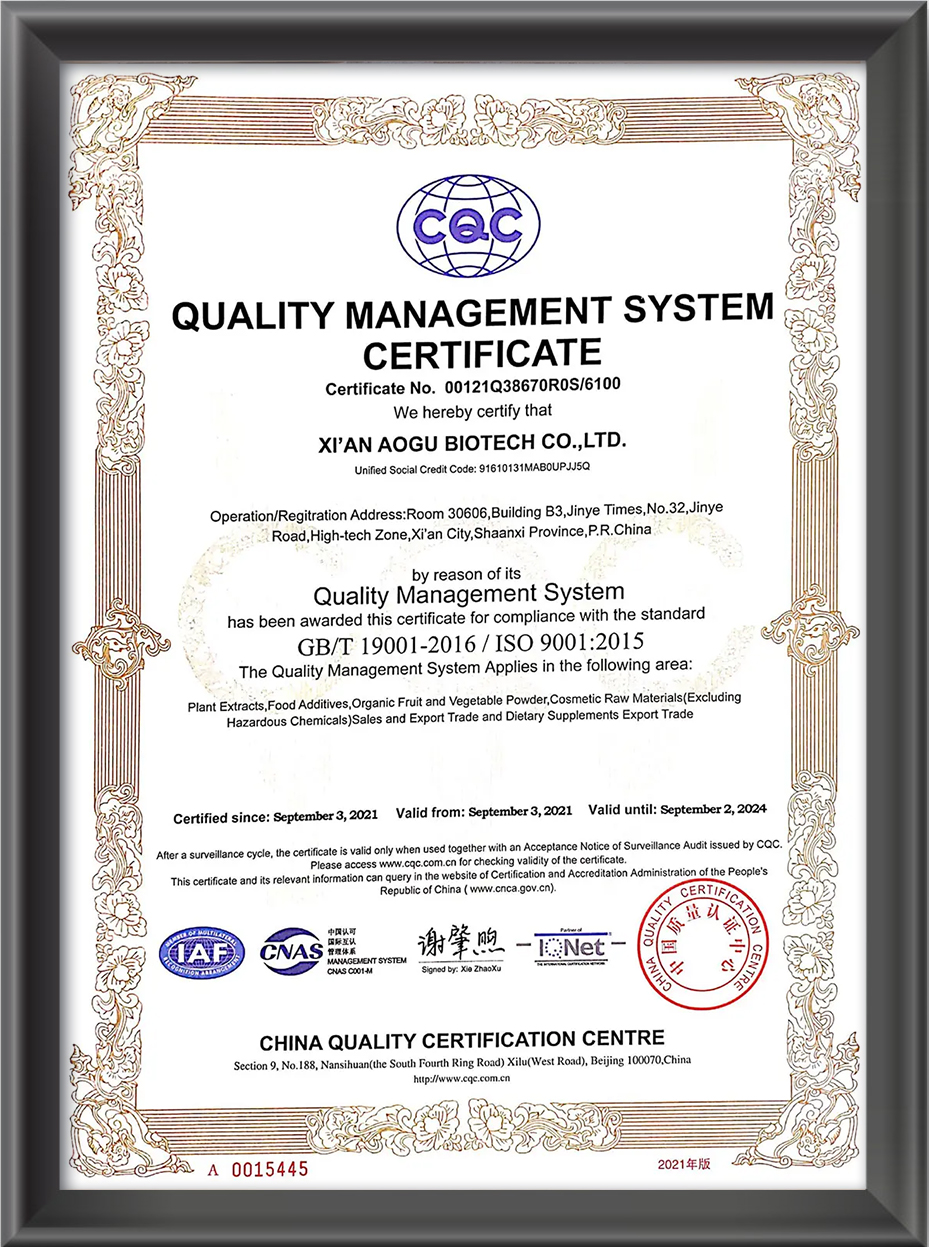
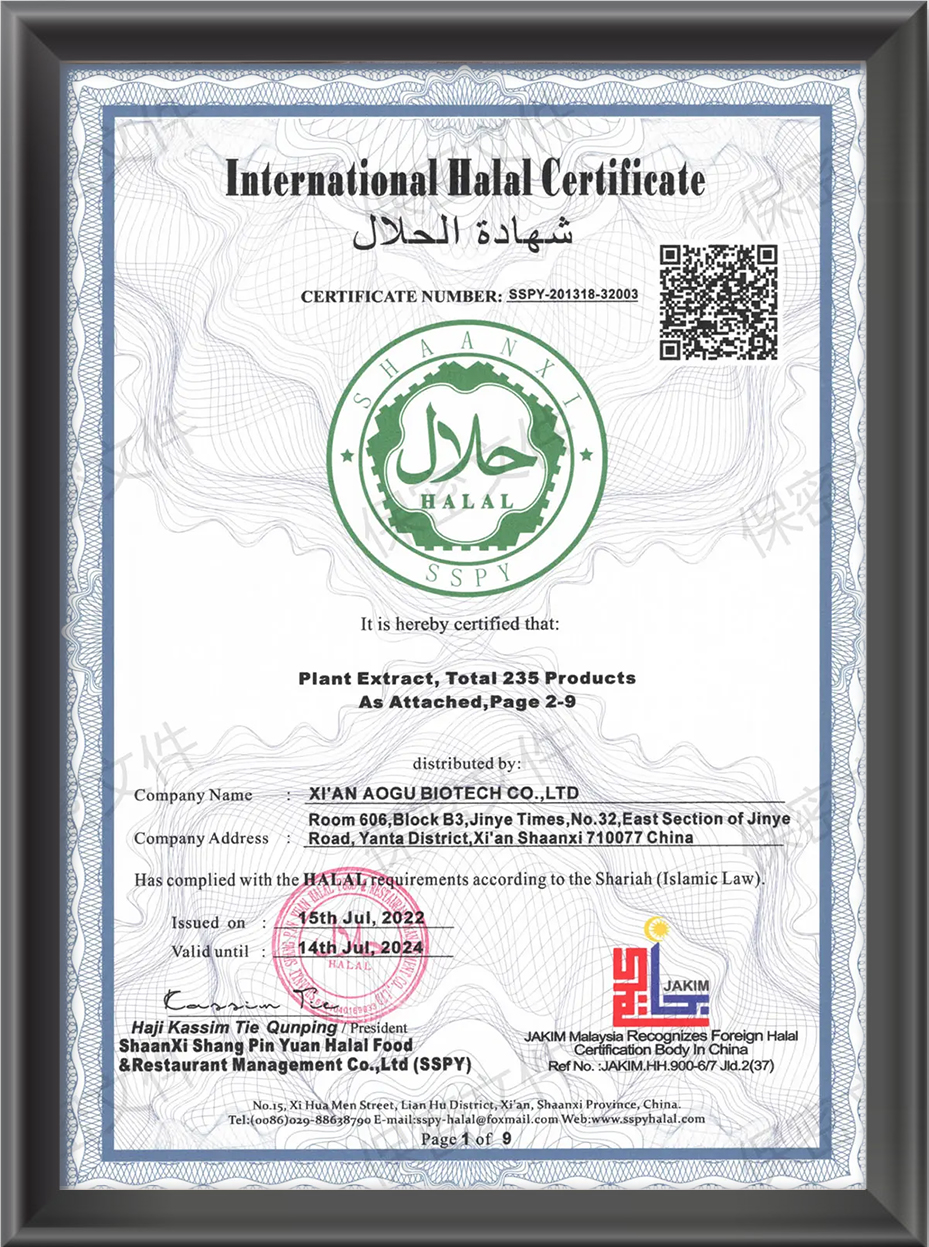
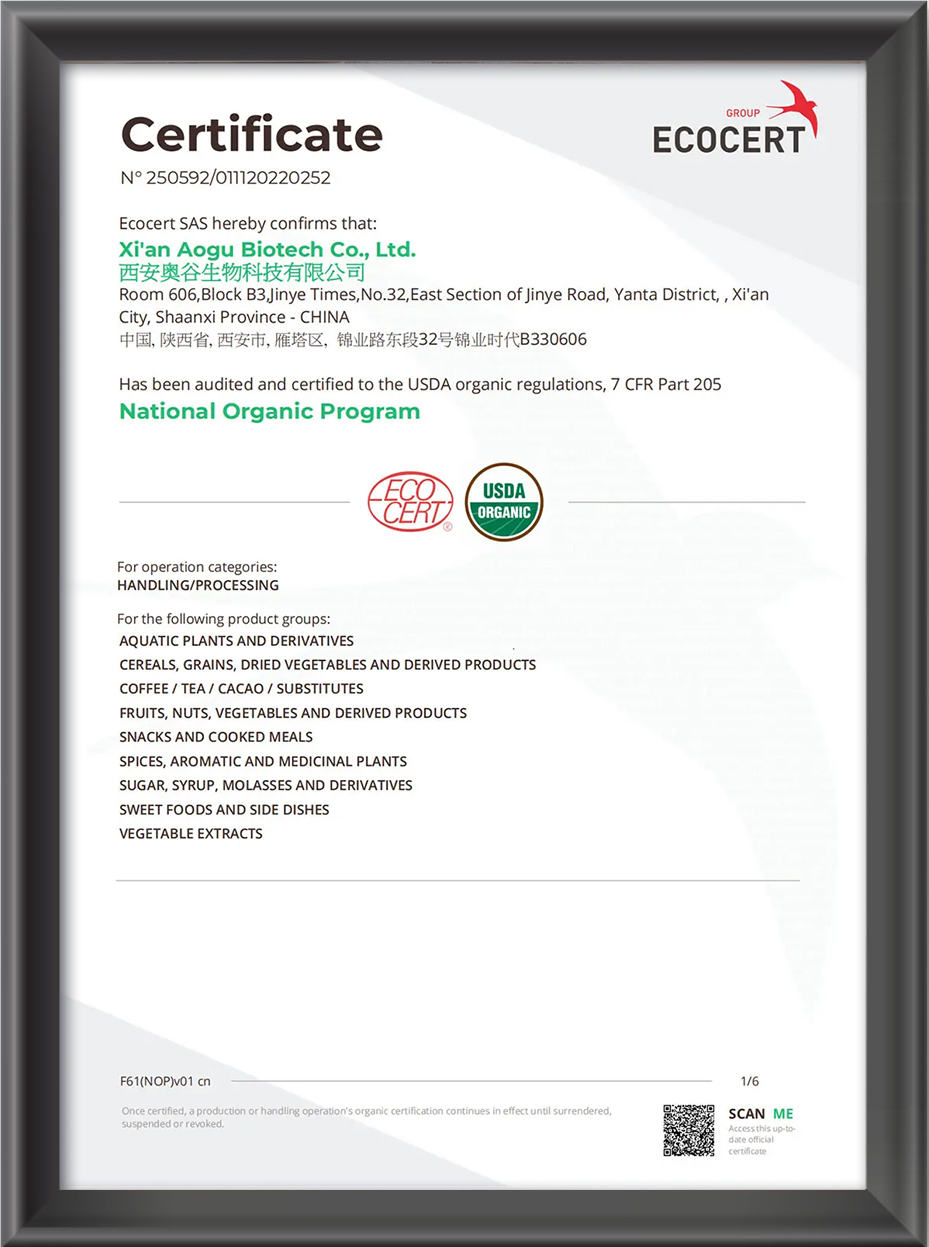
Unwavering dedication to customer technical support, comprehensive regulatory filing dossier supply (COA, MSDS, ISO, HALAL, KOSHER).
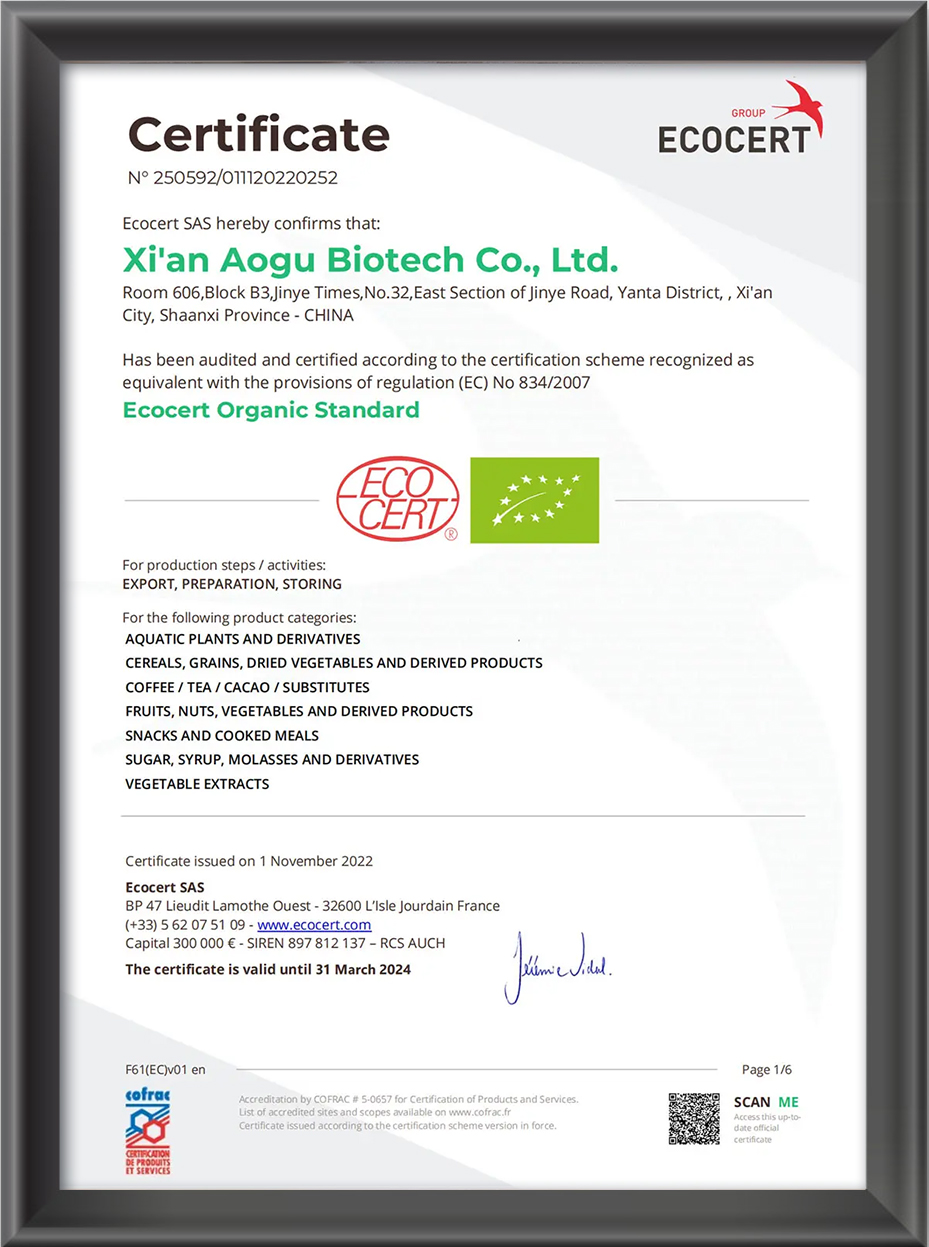
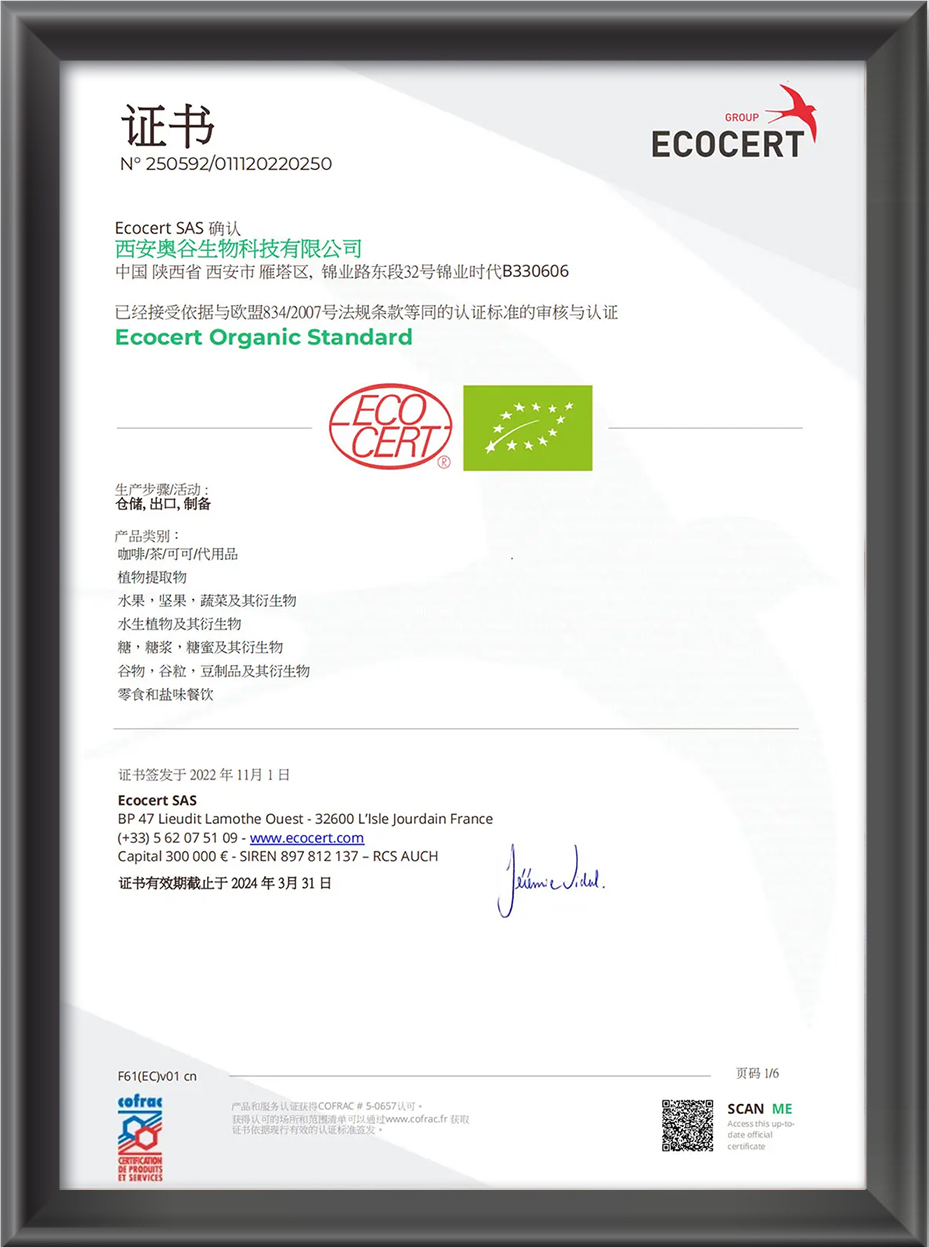
The future of industrial sugar synthesis lies at the intersection of Synthetic Biology and low-carbon processing technology. Aogebio LLC is currently researching recombinant enzyme immobilized matrix systems to boost biocatalytic yields by up to 35%, while simultaneously reducing thermal energy input by 20%.
Furthermore, expanding research into Trehalose's role in cellular repair pathways—specifically as a safe autophagy inducer for neuroprotective and skin-longevity products—positions our factory as a strategic partner for cutting-edge anti-aging brand innovators globally.
Complementary raw material solutions available for global wholesale supply and customized OEM blending.

 Aogebio Cosmetic